Hey there, thanks for popping by my corner of the web. I’m [your role here—like lead sales for explosive clad plates, but keep it casual], and I get tons of questions from folks in pressure vessel manufacturing: “Are explosive clad plates even worth the hype for my tanks, reactors, or heat exchangers?” It’s a fair question—pressure vessels aren’t your run-of-the-mill metal parts. They deal with extreme temps, corrosive fluids, and constant pressure swings, so cutting corners here can lead to big problems. Let’s break this down like we would over a coffee run, no stuffy jargon or corporate fluff. Explosive Clad Plates
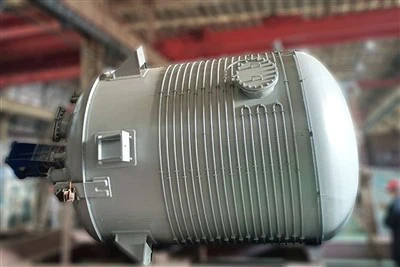
First, let’s cut to the chase: Explosive clad plates (ECP) absolutely are suitable for most pressure vessel applications—if you know what you’re getting, and how to spec it right. Let’s start with the basics, because a lot of people mix ECP up with other composite metals. Think of ECP as two (or sometimes more) metal layers fused so tight you can’t yank ’em apart without breaking one of ’em. The base layer is usually carbon steel—cheap, strong, perfect for holding pressure. The clad layer? It’s the fancy stuff that resists corrosion: stainless steel, alloy 600, titanium, even nickel alloys for super harsh environments. That combo is way cheaper than using a solid block of the clad metal alone, and way tougher than just welding two separate plates together.
Now, why does this matter for pressure vessels specifically? Let’s talk use cases. Most pressure vessels handle stuff like chemical processing, oil and gas, food and beverage, or pharmaceuticals. Each of these has its own corrosion headaches. For example, a vessel storing sulfuric acid might need a titanium clad layer—titanium doesn’t react with strong acids, and carbon steel takes the brunt of the internal pressure. If you used solid titanium? That’d cost 5–10 times more, and you don’t even need all that strength. Weld two separate plates together? The weld joint is always a weak point—corrosion can creep in there, or the joint might fail under pressure over time. ECP eliminates that gap entirely.
But wait, I know what you’re thinking: “I’ve heard horror stories about clad plates delaminating.” Yeah, but that’s almost always from bad manufacturing, not the technology itself. When we make ECP, we use precision explosive bonding—we don’t just set off random dynamite near two plates. The process is controlled: we prep the surfaces so there’s no oil, rust, or gunk between the layers, set the explosive charge at a calibrated angle and force, and the impact fuses the atoms of the two metals together. The result is a bond strength that’s higher than the tensile strength of the base metal, so delamination would mean the whole plate breaks, not just the layers pulling apart. Bad delamination happens when someone cuts corners: surfaces weren’t prepped, explosive force was too low, or layers were mismatched (like trying to bond aluminum and steel without a transition layer, which we always do for tricky metal pairs).
Let’s get real about pressure vessel standards, because this isn’t a “I say it works” deal. We work with ASME BPVC Section VIII, the code that governs pressure vessels in North America, and EN 13445 for Europe. Both have specific rules for ECP. ASME lets you use clad plates as pressure retaining components as long as the bond is tested—we do things like ultrasonic testing (UT) to check for voids, shear strength tests to make sure the bond holds, and even bend tests to make sure the plate doesn’t split when it’s shaped into a vessel’s curved shell. A lot of our clients used to use weld-overlay cladding, where you spray or weld the corrosion-resistant layer onto the base steel. But overlay has its own issues: the weld can have porosity, it’s thicker than needed, and it adds labor costs. ECP is more uniform, thinner, and faster to form—no extra welding after you get the plate.
Wait, let’s talk numbers to make this tangible. A client I worked with last year was making 15 pressure vessels for a fertilizer plant. They originally planned to use solid alloy 400 nickel, which would’ve cost them $120k total. We recommended ECP: carbon steel base, 3mm thick alloy 400 clad layer. The total cost? $45k. That’s a 62.5% savings, and the vessels passed all hydro pressure tests with zero issues. Six months later, they told us their competitor’s weld-overlay vessels had two corroded joints, but theirs were holding strong. That’s the kind of win I live for.
But it’s not all perfect—ECP isn’t for every pressure vessel. Let’s call out the caveats so you don’t waste your time. First, if your pressure vessel is super small, like a lab-scale reactor that only holds 100 PSI, ECP might be overkill. Solid carbon steel would work, and you won’t need the corrosion-resistant layer. Second, if you’re dealing with extremely high temperatures (above 1100°F for most common metal pairs), the bond can weaken—explosive clad is great for temps up to that threshold, but beyond that, you need a different bonding method or a transition metal. Third, if you need to drill tiny holes or do complex machining on the clad side, you have to be careful to not expose the base steel. For example, if you drill a hole all the way through the clad layer, you’ll have a spot where the corrosive fluid hits carbon steel—you have to cap that with weld or a plug. We train all our clients on that, no exceptions.
Another common question: “How long do ECP pressure vessels last?” That depends on the application, but we’ve got vessels that are 20 years old and still in use at chemical plants. A solid clad vessel from a sketchy supplier might last 5 years if the bond was bad, but a properly made ECP one? It’s built to match or exceed the lifespan of a solid carbon steel vessel, with the corrosion resistance of the top layer. I’ve seen clients switch from weld-overlay to ECP and cut their maintenance costs by 40% because they’re not constantly patching corroded joints.
Let’s address the elephant in the room: the cost of ECP vs solid metal. Yeah, ECP is more expensive than just plain carbon steel, but way cheaper than solid clad metal. Most pressure vessel manufacturers see a return on investment in 1–2 years because of lower material costs, less labor, and fewer maintenance repairs. If you’re building a vessel that’ll be in service for 15+ years, that savings adds up fast.
Now, let’s talk about how to get the right ECP for your pressure vessel. First, work with a supplier that does their own testing. Ask for UT reports, shear strength data, and proof they follow ASME or EN standards. A lot of cheap suppliers outsource bonding and skip tests, which is how delamination happens. Second, know your operating conditions: what’s the internal fluid? What’s the max pressure and temperature? What’s the corrosion rate you need to fight? That’ll tell you which clad metal to use—stainless for mild acids, titanium for strong ones, nickel alloys for high-purity environments like pharma. Third, don’t forget about forming. ECP is easy to roll into cylinders or bend into heads, but you have to make sure the supplier has experience forming clad plates—if they just treat it like plain steel, they can damage the bond.
I know a lot of pressure vessel makers are hesitant to switch from what they’ve always used. I get it—changing materials means reworking your welding processes, your testing protocols, even your inventory. But when we walk a client through the numbers, and show them real-world examples of vessels that have lasted decades with zero issues, that hesitation fades. Last quarter, a client in Texas came to us because their weld-overlay vessels were failing every 3 years. They switched to ECP, and their maintenance costs dropped so much they were able to take on a new project they couldn’t afford before.
At the end of the day, explosive clad plates aren’t a one-size-fits-all solution, but they’re ideal for most pressure vessel applications where corrosion and pressure are non-negotiable. They strike that perfect balance between strength, cost, and durability that other materials can’t match. If you’re currently dealing with corroded joints, overspending on solid clad metal, or worried about pressure vessel failure, let’s chat. We can walk through your specs, run some quick calculations, and show you how ECP fits your project. No sales pitch, just real talk about what works for your pressure vessels.

If you’re ready to talk through your needs, we’re here to help—reach out, and we’ll get back to you fast.
Mixing System References:
- ASME Boiler and Pressure Vessel Code, Section VIII: Division 1, Rules for Construction of Pressure Vessels. American Society of Mechanical Engineers, 2023.
- EN 13445-3:2021, Unfired pressure vessels – Part 3: Design. European Committee for Standardization, 2021.
- Wang, Y., et al. “Mechanical and Corrosion Properties of Explosive Clad Stainless Steel/Carbon Steel Plates for Pressure Vessel Applications.” Journal of Materials Engineering and Performance, vol. 29, no. 12, 2020, pp. 8167–8175.
- Bataille, F., et al. “Bond Strength Evaluation of Explosive Clad Plates for High-Pressure Chemical Reactors. Procedia Manufacturing, vol. 47, 2020, pp. 1212–1219.
Weihai Chemical Machinery Co., Ltd.
Weihai Chemical Machinery Co., Ltd. is one of the leading explosive clad plates manufacturers and suppliers in China. We warmly welcome you to buy OEM explosive clad plates from our factory. All customized products are with high quality and low price. For quotation, contact us now.
Address: Dongxin Road No.9, Zhangcun Town, Huancui District, Weihai City, China
E-mail: sales@weihaicm.com
WebSite: https://www.weihaicm.com/
